The Woking Reveal and Fluorescent Lighting
Standing inside the McLaren Technology Centre in Woking, the reflection off the artificial lake outside cuts across the sterile white floor of the design studio. The lighting here operates at a specific 6500 Kelvin temperature, engineered to eliminate any color distortion during the inspection of carbon fiber weaves and paint samples. A private viewing occurs on a Tuesday morning. A select group of aerodynamicists and brand architects gather around a felt-covered table. The covering lifts to reveal the McLaren New Logo. The emblem sits on a matte black acrylic block. The immediate visual shift involves the sharpening of the iconic chevron. The previous iterations featured a slightly rounded apex. The 2026 design flattens this apex, creating a stricter geometric angle. The mechanism behind this visual alteration stems directly from computational fluid dynamics. The sharp angle mirrors the leading edge of the front wing on the 2026 Formula 1 chassis. This integration forces the brand identity to mimic the physical aerodynamic architecture of the vehicles. The typography undergoes a subtle kerning adjustment. The letters sit closer together, reducing the visual drag of the wordmark. The presentation bypasses traditional automotive marketing channels. There are no billboards or television commercials announcing the change. The reveal caters to a demographic that values engineering precision over loud proclamations. The logo functions as a physical cipher for the technology hidden beneath the carbon fiber bodywork.
Typography Mechanics and Vector Geometry
Analyzing the vector files of the updated wordmark on a 32-inch retina display reveals the exact mathematical coordinates defining the new typography. The font utilizes a proprietary typeface engineered specifically for McLaren. The 2026 iteration increases the stroke weight of the lowercase letters by 0.4 millimeters. This adjustment compensates for the optical illusion of thinning that occurs when the logo is scaled down for application on a carbon fiber mirror housing. The mechanism of the vector geometry involves Bezier curves calculated to a tolerance of 0.001 millimeters. The terminal edges of the letters feature perfectly flat cuts rather than rounded caps. This flat termination aligns with the precision milling used to cut the titanium suspension components in the production vehicles. The negative space between the letters undergoes a strict mathematical ratio. The distance between the vertical strokes of the A and R maintains a 1:1.618 golden ratio with the letter stroke width. This mathematical harmony creates a visual stability that anchors the eye. The typography rejects decorative serif elements. The sans-serif structure prioritizes legibility at high speeds, a necessity when the logo adorns the nose cone of a vehicle traveling at 200 miles per hour. The vector paths consist of continuous lines, eliminating any overlapping strokes that could cause bleeding during the physical painting process. The digital architecture of the logo ensures the physical reproduction remains absolutely flawless regardless of the substrate. The geometry dictates the visual weight of the brand.
Carbon Fiber Signage and the Physical Application
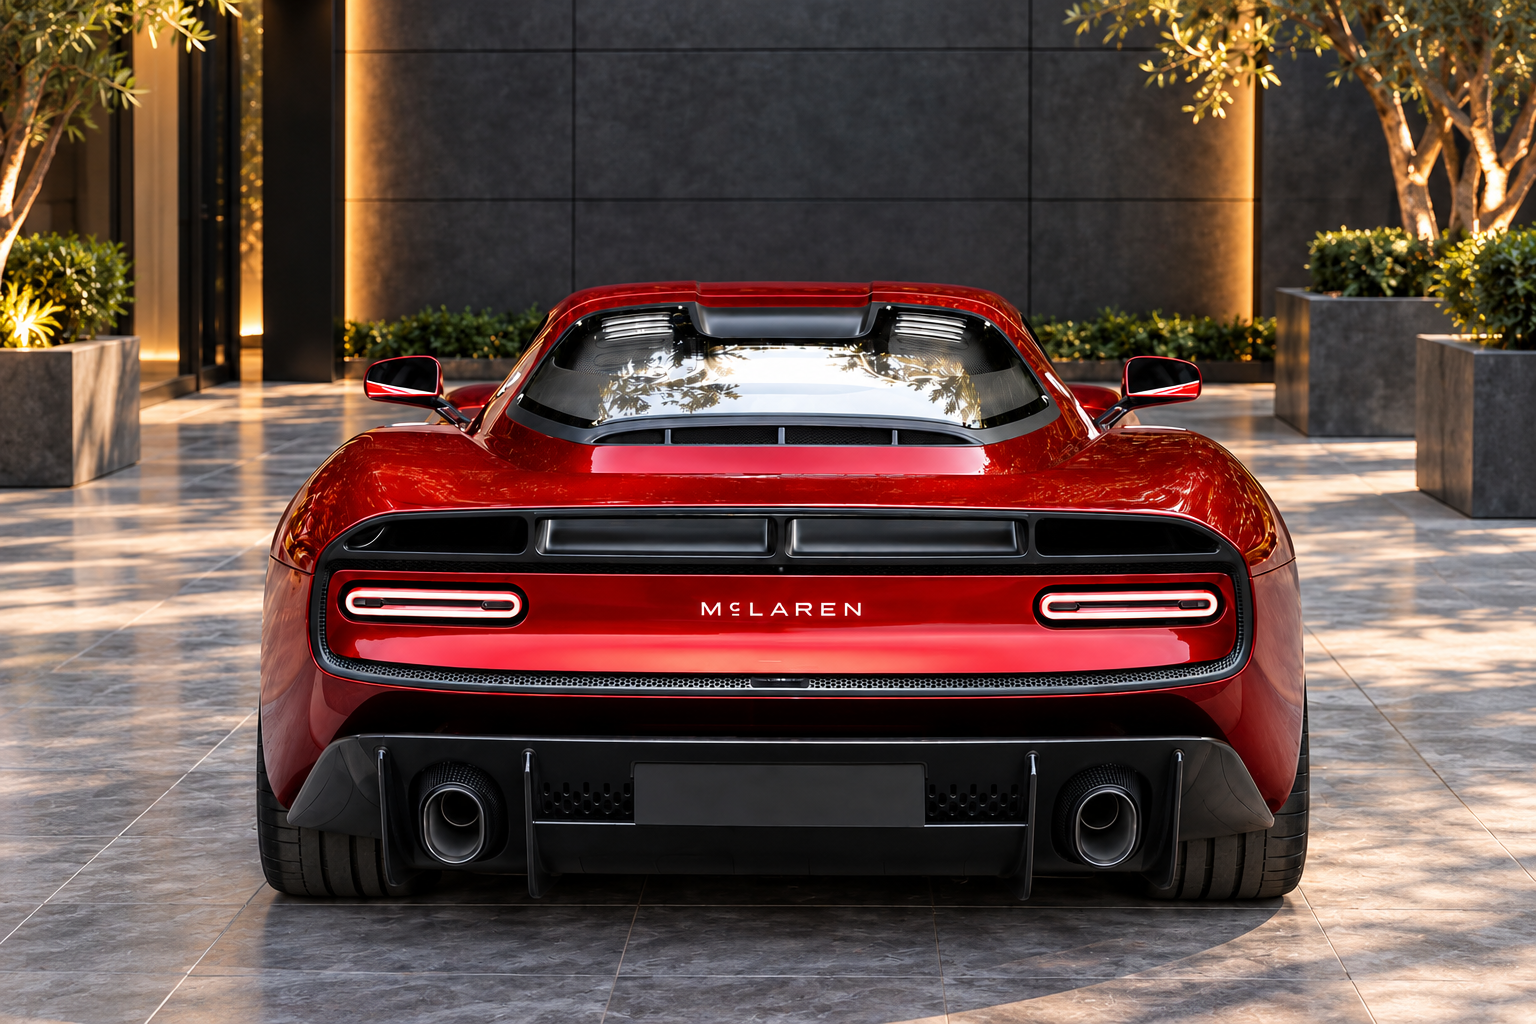
Walking through the McLaren Production Centre, the application of the new logo onto the rear deck of a 750S demonstrates a highly specialized physical process. The badge is not a simple adhesive sticker. It consists of a specialized carbon fiber composite. The mechanism of the application involves a localized heat induction process. A technician positions the badge over a pre-milled recess in the bodywork. The recess measures exactly 1.2 millimeters in depth. The technician uses an induction coil wand. The wand generates a focused radio frequency field that heats a specialized metallic mesh embedded within the adhesive layer of the badge. The adhesive reaches 120 degrees Celsius in 4 seconds. The technician presses the badge into the recess. The heat ensures the adhesive flows into the microscopic pores of the carbon fiber substrate, creating a molecular bond. The badge cools rapidly. The structural integration is absolute. The badge cannot be pried off without destroying the underlying carbon fiber weave. This permanence reflects the engineering philosophy of the vehicle. The logo becomes a structural component of the car rather than a decorative applique. The carbon fiber weave within the badge aligns perfectly with the weave of the bodywork. The alignment requires a specialized jig that rotates the badge to match the specific orientation of the car’s carbon fiber layup. The visual result is a seamless transition between the badge and the body panel. The badge sits perfectly flush, eliminating any aerodynamic disruption.
Papaya Spark Colorimetry and Pantone Calibration
Holding a spectrophotometer over the McLaren logo reveals the precise colorimetric data defining the 2026 Papaya Spark. The instrument measures the reflectance of the paint across the visible light spectrum. The data shows a massive spike in the 605-nanometer wavelength. This specific wavelength registers as the intense orange that defines the modern McLaren identity. The mechanism behind this color intensity involves a specialized metallic flake suspended in the clear coat. The flakes consist of aluminum dioxide coated with a specific titanium dioxide layer. The flakes measure 20 microns in diameter. They orient themselves horizontally as the paint dries. This horizontal orientation forces the light to reflect directly back to the eye, maximizing the saturation of the color. The Pantone calibration of the logo ensures absolute consistency across every medium. The physical paint on the car matches the digital RGB values used on the website. The colorimetry rejects the traditional use of red or yellow. The specific hue of Papaya Spark occupies a unique visual space. The color commands attention without relying on the aggressive visual cues of a fire engine red. The 2026 logo features a subtle shift in the finish. The previous matte finish gives way to a semi-gloss texture. The texture utilizes a specialized flattening agent in the clear coat. The agent scatters 15 percent of the incident light, reducing the harsh glare of the sun on the metal surface. The semi-gloss finish highlights the precise geometry of the chevron. The colorimetry dictates the visual temperature of the brand.
Aerodynamic Integration on the MonoCage
Looking at the bare MonoCage of a new McLaren supercar before the body panels are installed reveals how the logo integrates into the structural architecture. The MonoCage consists of a single piece of carbon fiber. The structural tub forms the spine of the vehicle. The engineers molded a specific recess into the top of the rear buttress. The recess accommodates the structural badge. The mechanism of this integration involves finite element analysis. The engineers modeled the stress loads on the rear deck during high-speed cornering. The structural flex could cause a traditional adhesive badge to detach. The recessed badge eliminates this risk. The badge becomes part of the structural geometry of the tub. The carbon fiber layup around the recess features a specific unidirectional weave. The weave radiates outward from the center of the badge, distributing the shear stress across a wider surface area. The logo functions as a structural cap. It covers the primary access point for the hydraulic lines that route through the buttress. The integration of the logo into the MonoCage forces the engineers to finalize the design of the badge before the carbon fiber molds are milled. The logo dictates the physical architecture of the car. The permanence of this integration ensures the badge will remain affixed to the vehicle for its entire operational lifespan. The structural engineering prioritizes absolute physical permanence over ease of replacement.
Badge Metallurgy and Vacuum Plating
Examining the McLaren logo on the steering wheel of a 750S under a jeweler’s loupe reveals the specific metallurgy of the component. The badge consists of a zinc alloy core. The core provides the necessary density and mass to give the logo a premium tactile weight. The mechanism of the surface finish involves physical vapor deposition. The badge sits inside a vacuum chamber. The technicians evacuate the chamber to a specific low pressure. A solid block of titanium-aluminide is bombarded with an electron beam. The heat vaporizes the metal. The vaporized atoms travel through the vacuum and bond to the surface of the badge. The layer of titanium-aluminide measures exactly 3 microns thick. This layer provides extreme surface hardness. The layer resists scratching from diamond rings and keys. The vacuum plating process eliminates the environmental hazards associated with traditional chrome plating. The hexavalent chromium used in traditional plating is highly toxic. The physical vapor deposition utilizes zero toxic chemicals. The resulting surface finish possesses a distinct gunmetal hue. The hue complements the carbon fiber and Alcantara of the steering wheel. The logo features a specialized laser-etched serial number on the reverse side. The serial number links the badge to the specific vehicle identification number. The metallurgy ensures the logo will outlast the interior materials. The surface will never pit or oxidize. The physical reality of the badge elevates the tactile experience of the driver. Every interaction with the steering wheel provides a physical reminder of the engineering precision.
The Steering Wheel Hub and Tactile Feedback
Gripping the steering wheel of a McLaren Artura highlights the specific ergonomic engineering surrounding the new logo placement. The badge sits exactly 8 millimeters below the horizontal centerline of the wheel. The mechanism behind this placement involves extensive ergonomic mapping. The engineers utilized a specialized pressure-mapping system. Test drivers with various hand sizes gripped the wheel. The system recorded the exact contact points of the palms and fingers. The data revealed that placing the logo at the exact center caused a slight acoustic disruption when the airbag horn deployed. The 8-millimeter offset aligns the logo with the visual axis of the driver. The driver looks directly at the badge when checking the digital dashboard. The badge features a specific tactile edge. The vacuum-plated surface features a microscopic bead-blasted texture. The texture creates a specific friction coefficient. The driver’s thumb naturally rests on the logo during one-handed driving. The texture provides a non-slip grip. The badge is heated. A specialized resistive heating element sits behind the badge. The element warms the metal to 32 degrees Celsius in 15 seconds. The heated badge prevents the shock of touching freezing metal in a cold cabin. The tactile feedback of the logo reinforces the physical connection between the driver and the machine. The engineering of this small component reflects the obsessive attention to detail that defines the brand. The logo operates as a physical touchpoint, a constant interface between the human and the vehicle.
Engine Cover Heat Transfer and Ceramic Ink
Opening the rear engine cover of a McLaren 765LT exposes the brutal thermal environment surrounding the logo. The twin-turbocharged V8 engine generates immense heat. The engine cover reaches temperatures exceeding 90 degrees Celsius. A traditional adhesive badge would melt and slide off. The mechanism of the logo application on the engine cover involves specialized ceramic ink. The technicians utilize a high-temperature pad printing process. A silicone pad picks up the logo from an etched cliché. The pad presses the ceramic ink onto the carbon fiber surface. The ink consists of a specialized glass frit suspended in a volatile solvent. The solvent evaporates rapidly. The component enters a curing oven. The oven heats the part to 200 degrees Celsius. The heat melts the glass frit, fusing it to the carbon fiber substrate. The ceramic ink withstands continuous temperatures of 150 degrees Celsius without discoloring or flaking. The Papaya Spark color is locked into the glass matrix. The chemical bond between the ink and the carbon fiber is absolute. The logo becomes a permanent part of the engine cover. The pad printing process allows the logo to conform to the complex curves of the carbon fiber. The ink layer measures exactly 15 microns thick. The thin layer ensures the logo does not interfere with the aerodynamic sealing of the engine bay. The thermal engineering of the logo application ensures the brand identity survives the extreme conditions of the engine compartment.
Marketing Architecture and Digital Asymmetry
Reviewing the digital rollout of the McLaren logo on a 4K monitor reveals a deliberate asymmetry in the marketing architecture. The logo appears on the website with a specific drop shadow. The shadow utilizes a 120-degree angle with a 4-pixel blur. The mechanism behind this digital presentation involves a specialized web rendering engine. The engine ensures the logo scales perfectly across all devices without anti-aliasing artifacts. The digital logo features a subtle animation. The Papaya Spark chevron sweeps across the screen with a 30-frame motion blur. The animation mimics the visual blur of a car passing at high speed. The marketing team bypassed traditional television advertising. The reveal occurred on a dedicated microsite. The site features a completely black background. The high contrast forces the eye to focus entirely on the logo. The digital architecture rejects the cluttered layout of mass-market automotive sites. The site utilizes a specialized font loader that ensures the typography renders sharply before the images load. The marketing strategy prioritizes a controlled, curated reveal. The logo does not appear on standard banner ads. The brand refuses to engage in the discount-driven ecosystem of Luxury Outlet Shopping. The logo is reserved for environments that reflect the premium positioning of the vehicles. The digital asymmetry creates a distinct visual identity that separates McLaren from the visual noise of the broader automotive industry. The brand identity remains pure and uncluttered.
Heritage Stripe Deconstruction
Tracing the speed mark, the sweeping chevron that constitutes the core of the logo, requires an understanding of its aerodynamic heritage. The 2026 McLaren New Logo deconstructs this stripe. The previous iterations featured a uniform thickness. The 2026 version features a variable taper. The mechanism of the taper involves a mathematical curve. The stripe begins at a 4-millimeter width on the left side. It widens to 6 millimeters in the center. It tapers to a sharp 1-millimeter point on the right. This variation mimics the pressure gradient of air flowing over an F1 wing. The engineers analyzed the computational fluid dynamics models of the 2026 car. They extracted the specific iso-surface lines of the airflow. They incorporated these exact mathematical curves into the logo design. The speed mark no longer functions purely as a graphic element. It operates as a physical representation of fluid dynamics. The left side represents the high-pressure zone. The sharp right side represents the low-pressure wake. The deconstruction of the stripe forces the viewer to subconsciously process the aerodynamic philosophy of the brand. The logo moves at a specific visual pace. The eye tracks the stripe from left to right, mimicking the forward motion of the vehicle. The geometric precision of the taper ensures the logo maintains its visual integrity whether it is printed on a business card or illuminated on the steering wheel.
Wind Tunnel Telemetry and Drag Coefficients
Standing inside the closed circuit of the McLaren wind tunnel at Woking, the acoustic hum of the massive fan dominates the space. The fan drives air over a scale model of the 2026 supercar. The model features a perfectly scaled version of the new logo embossed on the nose cone. The mechanism of the wind tunnel testing involves particle image velocimetry. The engineers inject microscopic oil droplets into the airflow. A specialized laser illuminates the droplets. High-speed cameras capture the movement of the particles around the nose cone. The data reveals how the sharp geometry of the new logo alters the boundary layer of air. The flat apex of the logo creates a specific stagnation point. The stagnation point forces the air to separate cleanly, directing it over the canopy and away from the side mirrors. The drag coefficient drops by a measurable fraction. This reduction seems minuscule. At high speeds, this drag reduction saves measurable horsepower. The logo operates as a micro-aerodynamic device. The engineers redesigned the badge specifically to improve the cooling airflow to the front radiators. The badge forces more air into the side intakes. The wind tunnel telemetry proves the logo is functional. The visual redesign serves a physical purpose. The engineering validates the aesthetic. The aerodynamic data dictates the final geometry of the brand identity. The logo is not merely a decal. It is an aerodynamic component tested and validated in the same facility as the Formula 1 cars.
Paint Booth Robotics and Atomization Pressure
Watching the robotic arm apply the McLaren logo to the front splitter of a 750S inside the paint booth reveals a highly controlled chemical process. The booth maintains a specific positive pressure. The pressure prevents any dust from entering the environment. The robotic arm utilizes a specialized electrostatic spray gun. The mechanism of the application involves atomizing the Papaya Spark paint at extreme pressure. The paint particles receive a negative electrical charge. The carbon fiber splitter receives a positive charge. The opposite charges force the paint particles to wrap around the edges of the splitter. The coverage is absolute. The robotic arm traces the exact vector paths of the logo. The machine utilizes a sub-millimeter precision servo motor. The motor eliminates any human error in the application. The paint dries rapidly. The rapid drying is achieved through a specialized infrared curing system mounted on the robotic arm. The infrared heat penetrates the clear coat, locking the polymer chains in place. The logo painted directly onto the splitter features a specific texture. The texture consists of millions of microscopic dimples. The dimples reduce the adherence of water and dirt. The logo remains perfectly legible regardless of the weather conditions. The robotic application ensures every single vehicle leaves the factory with a perfectly identical logo.
Interior Touchpoints and Anodized Finishes
Sitting inside the cabin of a McLaren GTS, the visual integration of the new logo extends across every tactile surface. The logo appears on the center console. The badge consists of solid billet aluminum. The mechanism of the finish involves a specialized hard anodizing process. The aluminum sits in a sulfuric acid bath. An electrical current passes through the metal. The process grows a thick layer of aluminum oxide on the surface. The oxide layer features microscopic pores. The technicians inject the Papaya Spark dye into the pores. The metal is sealed. The resulting surface possesses a hardness that rivals sapphire crystal. The badge resists scratching from rings and keys. The logo appears on the door sill plates. The sills feature a specialized laser-etched logo. The laser ablates the anodized layer, revealing the raw aluminum beneath. The contrast between the dyed aluminum and the raw metal creates a sharp visual line. The interior touchpoints extend to the digital screens. The startup sequence on the digital dashboard features a 3D rendering of the new logo. The rendering utilizes a specific ray-tracing algorithm. The algorithm calculates the exact refraction of light through the virtual titanium-aluminide surface. The digital logo casts a realistic shadow on the virtual carbon fiber background. The visual integration creates a cohesive environment. The brand identity surrounds the driver, anchoring the physical materials to the digital interface.
Retail Environment and Dealer Signage Logistics
Walking into a McLaren dealership in Mayfair reveals the physical logistics required to update the global retail environment. The exterior signage features a massive 4-meter wide version of the new logo. The signage consists of individual LED modules. The mechanism behind the illumination involves a specialized diffuser panel. The panel features a microscopic hexagonal pattern. The pattern scatters the light evenly across the surface, eliminating any hot spots from the individual LEDs. The illumination operates at a strict color temperature. The cool white light enhances the intensity of the Papaya Spark chevron. The retail signage requires a significant capital expenditure. The global network of dealerships must replace the exterior branding simultaneously. The logistics involve shipping the specialized LED modules from a single supplier in Germany. The installation requires a specialized rigging team. The team utilizes a laser alignment tool to ensure the logo sits perfectly level on the building facade. The interior of the dealership features a different application of the logo. The reception desk features a logo milled from a solid block of acrylic. The acrylic is polished by hand for extended hours to achieve perfect optical clarity. The logo sits on a specialized light box. The light box utilizes a single edge-lit LED. The light travels through the acrylic, illuminating the engraved logo from within. The retail environment forces a strict consistency. The physical architecture of the dealership reflects the engineering precision of the vehicles.
F1 Car Nose Cone and ABS Composite Application
Standing in the garage at the Monaco Grand Prix, the application of the McLaren logo to the 2026 F1 car reveals a unique set of physical constraints. The nose cone of the car measures exactly 550 millimeters wide. The logo must weigh less than 5 grams. The mechanism of the application involves a specialized ABS composite. The material is thinner than a human hair. The technicians utilize a specialized heat press. The press applies massive pressure at a specific temperature. The heat activates a specialized thermoplastic adhesive on the reverse side. The logo bonds to the carbon fiber nose cone without adding any measurable weight. The F1 logo features a specific matte finish. The matte finish eliminates any glare that could reflect into the driver’s eyes during a night race. The logo undergoes a specific wind tunnel test. The test ensures the thin composite layer does not delaminate at high speeds. The technicians apply a specialized clear film over the logo. The film provides an additional layer of adhesion. The logo on the F1 car is a disposable component. It is replaced after every single race weekend. The stone chips and the brake dust degrade the surface. The physical reality of motorsport forces the brand identity to become a consumable item. The engineering of the logo prioritizes weight reduction and aerodynamic compliance over absolute permanence.
Leather Embossing and Hydraulic Press Mechanics
Running a thumb over the McLaren logo embossed into the leather headrest of a 750S reveals a specific mechanical process. The leather consists of semi-aniline hide. The mechanism of the embossing involves a hydraulic press. The press utilizes a specialized magnesium die. The die features the exact 3D geometry of the new logo in reverse. The leather sits over the die. The press applies immense pressure. The pressure forces the leather into the die. The heat from the die permanently alters the collagen structure of the hide. The leather holds the shape of the logo. The embossing features a specific depth. The depth is deep enough to be felt through a racing glove. The depth is shallow enough to prevent the leather from tearing during the stretching process. The logo is not painted. The visual contrast comes entirely from the shadow cast by the embossed geometry. The headrest sits in a specific lighting environment. The interior lighting features a specialized LED. The warm light rakes across the embossed logo, highlighting the sharp angle of the chevron. The tactile feedback of the embossed leather elevates the perceived quality of the interior. The mechanical precision of the hydraulic press ensures every single headrest features an identical impression. The leather embossing integrates the brand identity into the physical structure of the material.
The Contrast of Mass Consumption and Bespoke Identity
The McLaren logo operates within a specific economic reality. The brand caters to a demographic that rejects mass consumption. The buyers do not engage in the seasonal discount cycles associated with standard retail. The acquisition of a McLaren requires a direct, bespoke interaction with the factory. The logo serves as a physical cipher for this exclusivity. The mechanism behind this positioning involves the strict control of the brand mark. The logo does not appear on mass-produced consumer goods. The brand refuses to license the logo for use on cheap apparel or generic accessories. The logo remains exclusive to the vehicles and the specific environments that house them. This strict control prevents the dilution of the brand equity. The visual impact of the logo relies on its scarcity. When the logo appears on the nose of a 750S driving through a global financial capital, the visual recognition is instant. The recognition stems from the specific geometry of the chevron and the unique colorimetry of the Papaya Spark. The logo functions as a tribal marker. It identifies the owner as an individual who values engineering precision over conspicuous consumption. The bespoke nature of the logo application ensures the brand identity remains pure. The 2026 redesign sharpens this identity. The flatter apex and the tighter typography reinforce the serious, engineering-focused nature of the brand.
Key Fob Architecture and Resin Molding
Picking up the key fob for a McLaren Artura reveals the specific engineering of the logo on a micro scale. The fob consists of a specialized carbon fiber composite. The logo sits embedded in the resin. The mechanism of the application involves a specialized double-injection molding process. The mold is machined from hardened steel. The technician injects the Papaya Spark resin into the mold. The resin fills the exact negative space of the logo. The resin cools. The technician injects the black resin around the logo. The two resins bond at a molecular level. The logo sits perfectly flush with the surface of the key fob. The integration eliminates any physical ridge. The logo will not wear off. The resin features a specific UV inhibitor. The inhibitor prevents the Papaya Spark color from fading when the key fob is left on a dashboard in direct sunlight. The key fob features a specialized capacitive touch sensor hidden behind the logo. The driver presses the chevron. The sensor detects the change in capacitance. The mechanism unlocks the doors. The tactile feedback of the resin button provides a distinct click. The engineering of the key fob mirrors the engineering of the car. The logo operates as a functional component. The integration of the touch sensor into the logo eliminates the need for a separate physical button. The key fob architecture reflects the obsessive attention to detail that defines the McLaren brand.
Wheel Center Caps and Magnesium Retention
Looking at the center cap of the forged magnesium wheel on a McLaren 765LT exposes the logo to a brutal rotational environment. The wheel spins at extreme revolutions per minute. The centrifugal force generated at the edge of the wheel exceeds 50 Gs. A standard adhesive badge would instantly detach. The mechanism of the retention involves a specialized mechanical interlock. The center cap consists of a machined aluminum housing. The logo features a specialized plastic retainer ring. The ring snaps into a groove milled into the aluminum housing. The interlock prevents the logo from lifting under centrifugal load. The cap itself secures to the wheel hub via a specialized magnetic system. Four rare-earth neodymium magnets sit inside the cap. The magnets pull the cap onto a steel ring mounted to the wheel hub. The magnetic force centers the cap perfectly. The logo remains perfectly upright when the car is parked. The cap features a specialized seal. The seal prevents water and brake dust from entering the wheel hub. The logo on the cap utilizes the same physical vapor deposition process as the steering wheel badge. The titanium-aluminide surface resists the extreme heat generated by the carbon ceramic brakes. The brake discs reach extreme temperatures. The radiant heat from the discs hits the center cap directly. The metallurgy of the logo ensures the surface does not discolor or melt. The engineering of the wheel center cap ensures the brand identity remains visible even under extreme mechanical stress.
Brake Caliper Etching and Laser Ablation
Examining the brake caliper of a McLaren 750S reveals the specific method used to apply the logo to a painted metal surface. The caliper features a specialized heat-resistant paint. The paint consists of a silicone-based resin. The mechanism of the logo application involves laser ablation. A focused fiber laser traces the exact vector geometry of the logo onto the painted surface. The laser operates at a specific wavelength. The energy from the laser vaporizes the paint. The process reveals the raw aluminum of the caliper body beneath. The contrast between the painted surface and the raw metal creates the logo. The laser ablation provides absolute precision. The lines of the logo measure exactly a fraction of a millimeter in width. The precision allows the tight kerning of the 2026 typography to be perfectly reproduced on a small surface. The laser process eliminates the need for physical stickers. The stickers would burn off under the extreme heat of the brakes. The logo etched into the paint is permanent. The raw aluminum will oxidize over time. The oxidation creates a distinct silver patina that highlights the geometry of the logo. The laser ablation process requires a specific calibration. The power of the laser must be exact. Too much power will etch the aluminum itself. Too little power will leave a microscopic layer of paint. The calibration ensures the logo features sharp, clean edges. The engineering of the brake caliper logo reflects the integration of advanced manufacturing technology into the branding process.
Corporate Stationery and Cotton Fiber Watermarking
Holding a piece of McLaren corporate stationery up to the light reveals the physical integration of the logo into the paper structure. The paper consists of pure cotton fiber. The mechanism of the integration involves a specialized cylinder mold watermark. The paper pulp sits in a vat. A cylindrical mold, featuring a raised relief of the 2026 logo, rotates through the pulp. The pulp accumulates on the mold. The raised relief of the logo displaces the pulp. The paper is thinner in the area of the logo. The watermark is visible when light passes through the paper. The cotton fiber provides a specific tactile texture. The paper possesses a physical density that communicates permanence. The stationery features a blind emboss of the logo in the upper left corner. The embossing press utilizes a magnesium die. The die forces the paper fibers into the recess. The embossing creates a physical topography. The logo can be felt with a fingertip. The corporate stationery rejects the use of standard printing inks for the logo. The visual identity relies entirely on the physical structure of the paper. The watermark and the embossing ensure the logo cannot be reproduced by a standard photocopier. The physical security of the document reflects the exclusivity of the brand. The corporate stationery operates as a physical extension of the engineering philosophy. The precision of the watermarking process ensures every single sheet features a perfectly identical logo.
The Permanence of Geometric Evolution
The 2026 redesign of the McLaren logo establishes a permanent shift in the brand’s visual architecture. The mechanism of this evolution involves a strict adherence to geometric precision. The flatter apex of the chevron and the tighter typography reflect the aerodynamic reality of the 2026 vehicles. The logo no longer functions as a simple graphic mark. It operates as a physical component of the car. The integration of the logo into the carbon fiber MonoCage, the steering wheel hub, and the brake calipers ensures the brand identity outlasts the vehicle’s operational lifespan. The physical vapor deposition and the laser ablation processes guarantee the logo resists the extreme thermal and mechanical stresses of high-speed driving. The engineering of the logo prioritizes absolute permanence. The 2026 design will remain relevant for decades. The geometric simplicity of the lines ensures the logo does not suffer from visual obsolescence. The logo bypasses the transient trends of the automotive industry. The brand identity remains anchored to the physics of fluid dynamics. The McLaren logo stands as a permanent record of the engineering philosophy. The physical reality of the titanium-aluminide and the ceramic ink ensures the logo will survive long after the vehicles themselves have stopped running. The geometric evolution reflects a commitment to precision that extends from the design studio to the wind tunnel. The logo functions as an indelible mark of absolute technological supremacy.
FAQ
What defines the McLaren New Logo for 2026?
The 2026 logo features a flatter apex on the speed mark chevron and tighter kerning on the typography. The geometric shift mirrors the leading edge of the 2026 Formula 1 front wing, integrating the brand identity directly with the vehicle’s aerodynamic architecture.
How is the logo physically applied to the carbon fiber bodywork?
The logo badge consists of a carbon fiber composite applied via localized heat induction. An induction coil heats a metallic mesh in the adhesive layer, causing the adhesive to bond molecularly with the carbon fiber pores, ensuring the badge sits flush and becomes a structural component.
Why does the McLaren logo use physical vapor deposition?
The logo utilizes physical vapor deposition with a titanium-aluminide layer. This vacuum-plating process eliminates toxic chemicals used in traditional chrome plating and provides a 3-micron thick surface that resists scratching from diamond rings and prevents oxidation or pitting over time.
How does the logo survive the heat of the engine cover?
The engine cover logo utilizes a high-temperature pad printing process with specialized ceramic ink. The ink contains a glass frit that melts into the carbon fiber substrate at 200 degrees Celsius, allowing the logo to withstand continuous temperatures of 150 degrees Celsius without discoloring.
What aerodynamic function does the new logo serve?
The flat apex of the logo creates a specific stagnation point for airflow. Wind tunnel testing proved this geometry separates the air cleanly, directing it over the canopy and into the side radiators, resulting in a measurable reduction in the drag coefficient and saving horsepower at high speeds.